 English
 Español
 Français
 Deutsch
 Português (Brasil)
 Русский
 العربية
Steel Penstock Manufacturer | Custom Steel Penstock for Hydropower Projects
 China
Supplier's customization ability
- Drawing-based customization
- Sample-based customization
- Full customization
Minimum order quantity: 1 ton
Shipping total: To be negotiated
- Lead time:
- confirmed with the quotation
- Packaging:
- standard export packing
- Samples:
- available on request
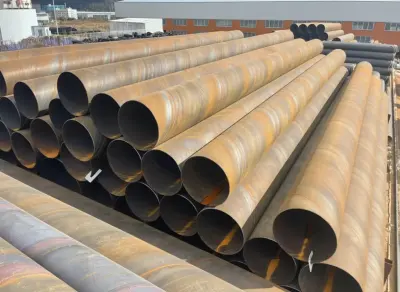
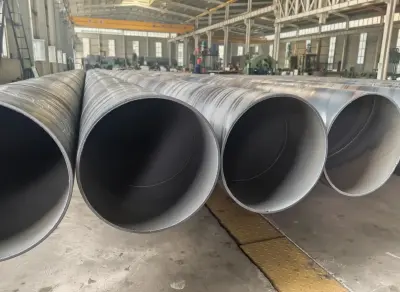
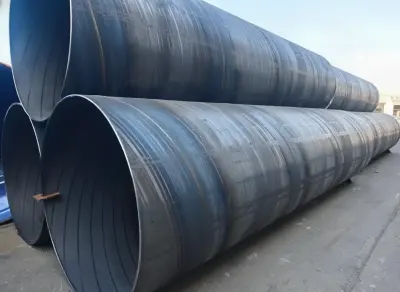
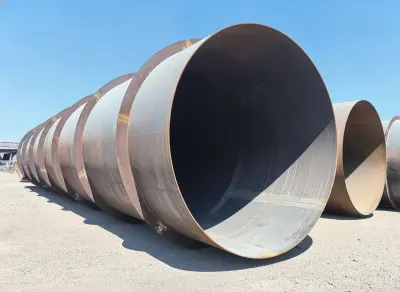
Product details
Steel Penstock Technical Specifications
| Parameter | Steel Penstock Specification |
|---|---|
| Product Name | Steel Penstock |
| Product Type | Welded steel pressure pipe for hydropower and water conveyance systems |
| Base Material | Carbon steel or high-strength low-alloy steel |
| Typical Steel Grades | ASTM A36, ASTM A572 Grade 50, ASTM A516 Grade 60/70, EN 10025 S275JR/S355JR, or equivalent |
| Outside Diameter | Customized according to flow capacity and project drawings |
| Wall Thickness | Customized based on diameter, internal pressure, steel grade, corrosion allowance, and design code |
| Pipe Length | Typically 6-12 m per section; custom lengths available |
| Manufacturing Process | Plate rolling, longitudinal welding, forming, dimensional inspection, and surface treatment |
| Welding Method | Submerged arc welding (SAW), gas metal arc welding (GMAW), or shielded metal arc welding (SMAW) |
| Joint Type | Field-welded butt joint, flanged joint, sleeve joint, or custom connection |
| Design Pressure | Engineered according to operating pressure, surge pressure, vacuum conditions, and required safety factor |
| Design Standards | ASME Section VIII, ASME B31.4, AWWA M11, EN 13480, or project-specific standard |
| Dimensional Tolerance | According to applicable manufacturing standard and approved project specification |
| Internal Coating | Potable-water-grade epoxy, coal tar epoxy, polyurethane, cement mortar lining, or custom coating system |
| External Coating | Epoxy, polyurethane, zinc-rich primer, bituminous coating, or three-layer corrosion protection system |
| Surface Preparation | Abrasive blast cleaning to ISO 8501-1 Sa 2.5 or SSPC-SP 10 |
| Corrosion Allowance | Specified according to service environment and design life |
| Non-Destructive Testing | Visual testing, ultrasonic testing, radiographic testing, magnetic particle testing, or dye penetrant testing as specified |
| Pressure Testing | Hydrostatic or project-specified pressure test after fabrication or installation |
| Quality Documentation | Material certificates, welding procedure records, NDT reports, dimensional reports, coating reports, and pressure test records |
| Accessories | Bends, reducers, bifurcations, expansion joints, manholes, stiffener rings, supports, anchors, and flanges |
| Applications | Hydropower plants, dams, pumped-storage facilities, water supply networks, irrigation systems, and industrial water projects |
| Customization | Diameter, wall thickness, steel grade, pressure rating, coating, joint design, and accessories can be manufactured to project requirements |
Steel Penstock Manufacturer | Custom Steel Penstock for Hydropower Projects
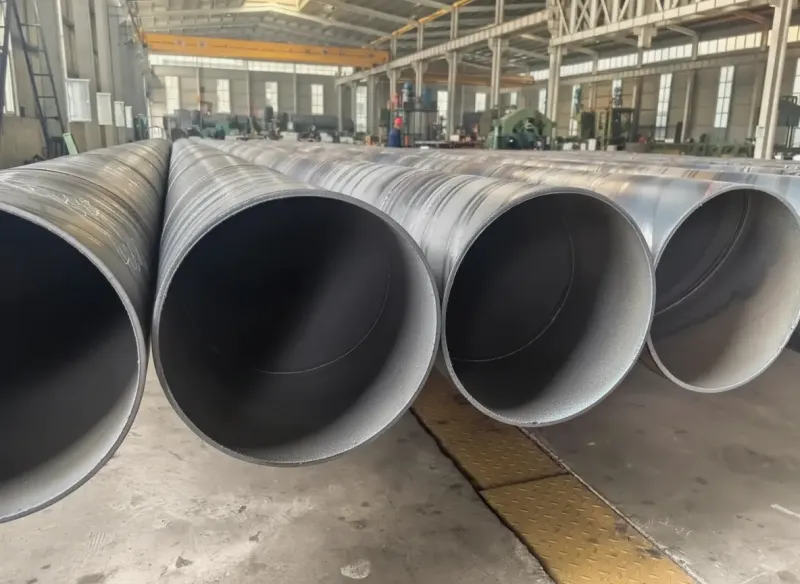
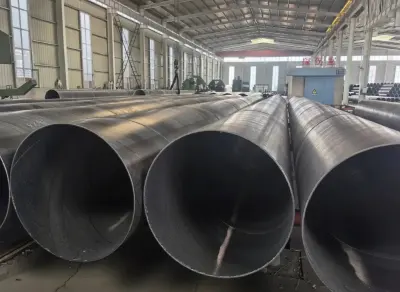
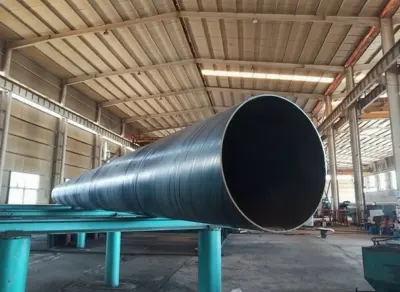
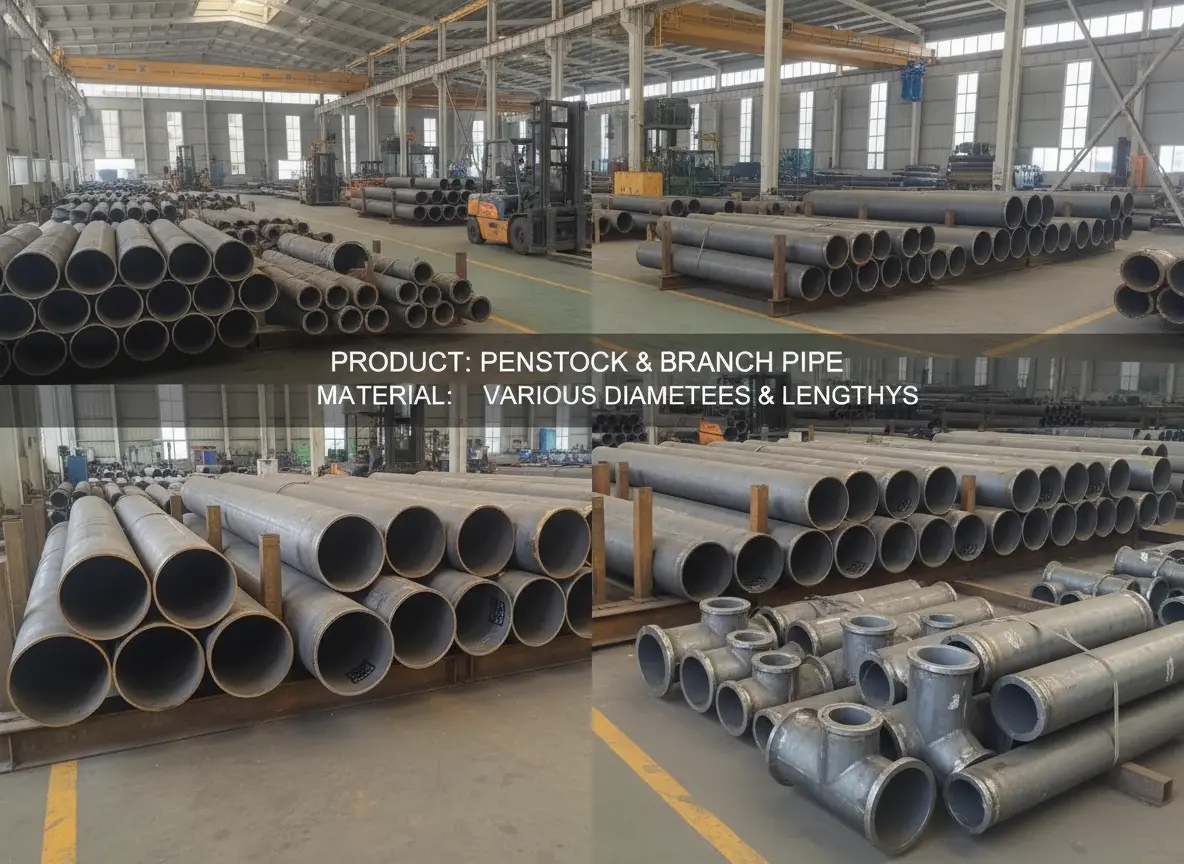
Steel penstock systems convey pressurized water from reservoirs, forebays, or surge facilities to turbines and other hydraulic equipment. Designed for hydropower developers, EPC contractors, civil engineering companies, and water infrastructure procurement teams, each fabricated pipeline must balance hydraulic efficiency, pressure resistance, weld integrity, corrosion protection, and practical site installation. A custom steel penstock can be engineered around the project head, transient pressure, route geometry, support arrangement, transport limits, and applicable inspection requirements. Reliable procurement therefore depends on more than nominal diameter and plate thickness; it requires coordinated design data, traceable materials, qualified fabrication procedures, documented testing, and a coating system matched to the operating environment.
Product Overview: Steel Penstock Design and Construction
A steel penstock is a welded pressure conduit used to carry water under static and dynamic hydraulic loads. It may be installed above ground on concrete or steel supports, buried with suitable external protection, embedded in concrete, or routed through tunnels. Hydropower installations commonly connect the penstock between an intake or forebay and a turbine inlet, while water supply and industrial projects may use similar fabricated steel pipe for gravity transmission, pumping, or pressure regulation.
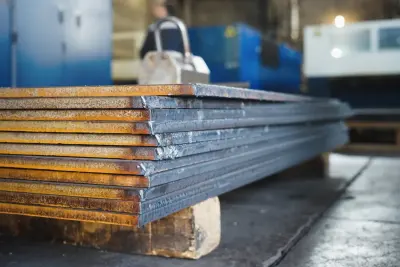
The main barrel is formed from structural or pressure-vessel-quality steel plate selected according to design pressure, minimum operating temperature, weldability, fabrication method, and the governing project specification. Commonly evaluated material frameworks include ASTM A36/A36M for carbon structural steel, ASTM A516/A516M for pressure vessel plate, EN 10025-2 for hot-rolled structural steels, and GB/T 1591 for high-strength low-alloy structural steels. The final grade must be approved by the project engineer; these standards are not automatically interchangeable because their chemical, mechanical, toughness, and testing requirements differ. Procurement teams comparing plate options can review [[INTERNAL_LINK]] before issuing a material requirement.
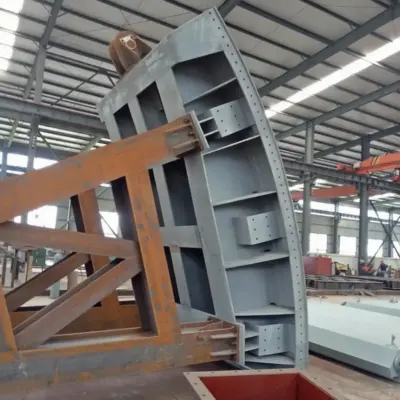
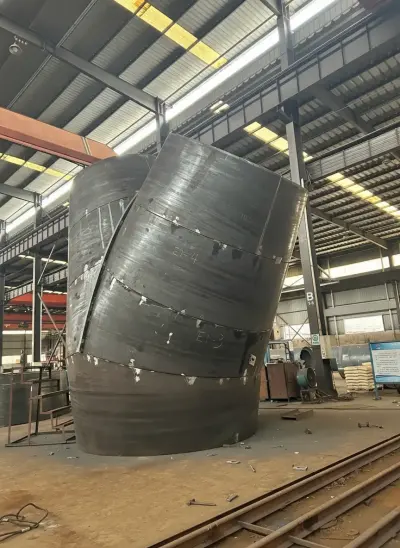
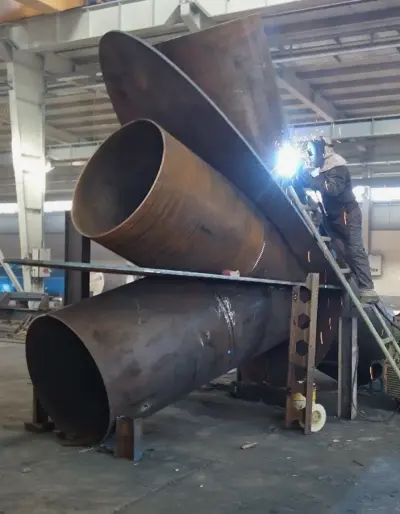
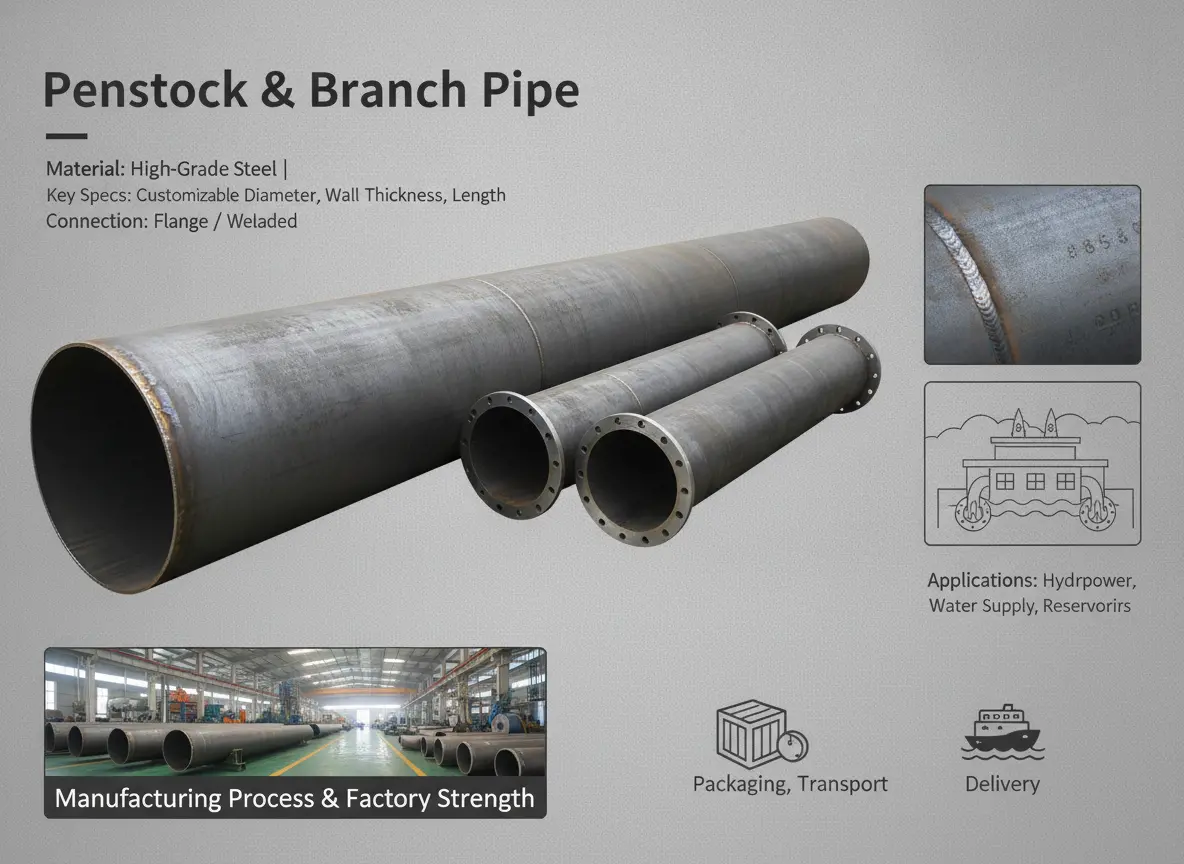
A fabricated steel penstock may include straight shells, elbows, reducers, bifurcations, manifolds, expansion joints, anchor rings, stiffener rings, flanges, manholes, drain connections, air-valve branches, and field closure pieces. The component arrangement depends on hydraulic analysis and the civil layout. Large-diameter sections are normally supplied in transportable lengths or segments, with circumferential field joints completed according to an approved erection and welding plan.
Key performance characteristics include pressure containment, controlled ovality, resistance to buckling where external pressure or vacuum can occur, and sufficient allowance for corrosion, handling, support reactions, and construction loads. Hydraulic transients deserve particular attention: rapid valve movement, turbine load rejection, pump shutdown, or air entrapment can create pressures significantly different from normal static head. Surge analysis and the selected design load combinations should therefore be completed before steel penstock plate thickness and reinforcement details are released for production. Related hydraulic engineering information is available at [[INTERNAL_LINK]].
Specifications & Standards for Steel Penstock Systems
Steel penstock specifications are project-specific. A complete inquiry should state the internal diameter, design flow, normal operating pressure, maximum transient pressure, minimum internal pressure, design temperature, alignment, bend radii, branch locations, support conditions, corrosion allowance, coating requirements, and required design life. The manufacturer also needs to know whether sections will be shop assembled, shipped as complete cans, delivered as split shells, or fabricated partly at the construction site.
Recognized references include AWWA M11, Steel Pipe: A Guide for Design and Installation, for engineering principles applicable to steel water pipe; ASCE Manual of Practice No. 79, Steel Penstocks, for penstock design and construction guidance; and EN 10224 for non-alloy steel tubes and fittings used in water and other aqueous liquid conveyance. Applicable requirements must be identified in the contract because these documents have different scopes and do not replace project-specific hydraulic and structural calculations.
| Specification Item | Typical Procurement Requirement | Relevant Reference or Verification |
|---|---|---|
| Internal diameter | Defined by hydraulic design and turbine or valve interface | Approved drawings and dimensional inspection |
| Plate material | Selected for strength, toughness, weldability, and temperature | ASTM A36/A36M, ASTM A516/A516M, EN 10025-2, or GB/T 1591 as specified |
| Wall thickness | Calculated for pressure, transients, external loads, buckling, and corrosion allowance | ASCE Manual No. 79, AWWA M11, and project design criteria |
| Pipe geometry | Diameter, length, roundness, end preparation, and fit-up tolerances | Approved fabrication drawings and contract tolerances |
| Welding | Qualified procedures, qualified personnel, controlled consumables, and documented parameters | AWS D1.1/D1.1M or ISO 15614-1 and ISO 9606-1, as contractually applicable |
| Non-destructive testing | Method and examination percentage based on joint category and project risk | ISO 17635 with applicable RT, UT, MT, or PT standards |
| Pressure or leak testing | Test pressure, duration, medium, restraints, and acceptance criteria defined by the engineer | Approved inspection and test plan |
| Corrosion protection | Interior lining and exterior system selected for immersion, atmosphere, soil, or concrete exposure | ISO 12944 series, AWWA C210, or another specified coating standard |
The following table gives examples of minimum yield strength values associated with commonly considered plate grades. It is not a project material schedule. Strength can vary with grade, thickness, delivery condition, and edition of the standard, so purchasers must verify the current material standard and mill certificate before approval.
| Example Plate Grade | Reference Standard | Indicative Minimum Yield Strength | Procurement Note |
|---|---|---|---|
| ASTM A36 | ASTM A36/A36M | 250 MPa for applicable plate thickness ranges | Confirm thickness-dependent requirements and impact-test needs |
| ASTM A516 Grade 60 | ASTM A516/A516M | 220 MPa for applicable plate thickness ranges | Pressure-vessel-quality plate; specify delivery condition and toughness requirements |
| S275JR | EN 10025-2 | 275 MPa at lower thickness ranges | Yield strength decreases in defined thicker ranges; JR impact requirements apply |
| S355JR | EN 10025-2 | 355 MPa at lower thickness ranges | Confirm subgrade if lower-temperature toughness is required |
Welding documentation should identify the base material group, joint design, process, consumable classification, preheat or interpass limits, heat input controls, and repair procedure. Depending on the contract, welding procedure qualification may follow AWS D1.1/D1.1M or ISO 15614-1, while welder qualification may follow AWS requirements or ISO 9606-1. Examination planning can reference ISO 17635, but the drawing or inspection and test plan must still state which joints are examined, the method used, the acceptance level, and the responsible inspection party. Guidance on fabrication quality documentation can be linked through [[INTERNAL_LINK]].
Coating selection should reflect the actual exposure zone. The internal surface may require a lining suitable for continuous water immersion, while external surfaces may face atmospheric humidity, buried soil, tunnel condensation, or concrete encasement. ISO 12944 provides a framework for protective paint systems in atmospheric and immersion environments. AWWA C210 covers liquid-epoxy coating systems for the interior and exterior of steel water pipelines. Surface preparation grade, abrasive profile, dry-film thickness, curing conditions, holiday testing, repair materials, and field-joint treatment should all be written into the coating specification.
Applications of Steel Penstock Equipment
Hydroelectric power stations: The primary application is conveying water to Francis, Pelton, Kaplan, or other turbine arrangements. The steel penstock route may include steep slopes, tunnels, anchor blocks, bifurcations, and turbine inlet branches. Design pressure must account for both gross head and water-hammer effects. See [[INTERNAL_LINK]] for related hydropower steel components.
Small and medium hydropower schemes: Run-of-river and mountainous projects often need customized section lengths because access roads, lifting capacity, and erection areas are restricted. A sectional steel penstock can simplify transport, but it increases the importance of accurate match marking, field-fit control, and a documented site-welding sequence.
Pumped-storage facilities: Reversible flow, frequent operating cycles, rapid load changes, and high transient pressures can make fatigue assessment and hydraulic surge control important. Bifurcations, manifolds, and local reinforcement must be evaluated as part of the complete water-conveyance system rather than treated as isolated fittings.
Water transmission and irrigation: Fabricated steel pressure conduits are used where large diameter, route-specific fittings, or structural adaptability is required. Typical installations include reservoir outlets, pumping stations, irrigation networks, and raw-water transfer lines. Material and lining suitability must be confirmed for the conveyed water and local regulatory requirements.
Industrial hydraulic systems: Mines, processing plants, cooling-water networks, and other industrial facilities may require large welded steel pipelines with custom branches and supports. Fluid chemistry, solids content, flow velocity, abrasion, and shutdown conditions should be disclosed because they influence lining and wear-protection decisions. Additional water pipeline products are available through [[INTERNAL_LINK]].
How to Choose a Steel Penstock: Buying Guide
Begin with an engineering data sheet rather than a diameter-only request. The steel penstock supplier needs the design flow, static head, normal pressure range, maximum surge pressure, possible vacuum, temperature range, route profile, and interface dimensions. Provide drawings in a controlled revision format and identify which party is responsible for hydraulic analysis, structural calculations, support design, and field erection. Unclear responsibility boundaries are a frequent cause of drawing revisions and delayed approvals.
Material selection should be based on calculated stress, thickness, weldability, fracture toughness, operating temperature, and availability under the specified standard. A stronger grade does not automatically produce a more economical steel penstock because welding controls, forming limits, inspection requirements, and procurement availability can offset plate-weight savings. Require material test certificates traceable to heat numbers and state whether third-party review, additional impact testing, or supplementary ultrasonic examination of plate is required. Buyers researching inspection options can consult [[INTERNAL_LINK]].
Define dimensional and fabrication requirements clearly. Important details include shell length, longitudinal seam orientation, roundness tolerance, end mismatch, bevel geometry, temporary bracing, lifting points, stiffener position, flange drilling, and match marks. For split sections, request a trial-assembly method and a clear identification system. For field-welded sections, confirm whether the supplier provides backing details, closure plates, consumables, coating repair kits, erection drawings, or site supervision.
Certification requirements should be established before quotation. The requested dossier may include material certificates, approved drawings, design calculations, welding procedure specifications, procedure qualification records, welder qualification records, NDT reports, dimensional reports, coating batch records, dry-film-thickness reports, holiday-test results, and pressure-test documentation. If an independent inspection agency is involved, identify hold points and witness points in the inquiry so inspection time can be included in the production schedule.
MOQ should be treated as a commercial variable, not assumed from general market practice. A custom steel penstock often involves engineering, plate nesting, forming setup, welding qualification review, and coating preparation. The practical minimum order therefore depends on diameter, thickness, section length, total tonnage, fitting complexity, and whether material can be sourced with other production requirements. Ask the manufacturer to state the applicable MOQ and any engineering or tooling implications in the quotation.
Lead time also depends on approved drawings and material availability, not only workshop capacity. A realistic schedule should separate engineering review, buyer approval, plate procurement, fabrication, NDT, coating, curing, final inspection, packing, and dispatch. Late changes to branch locations, flange interfaces, design pressure, or coating specifications can affect both cost and delivery. A document-submittal schedule is useful for keeping technical approvals aligned with manufacturing milestones.
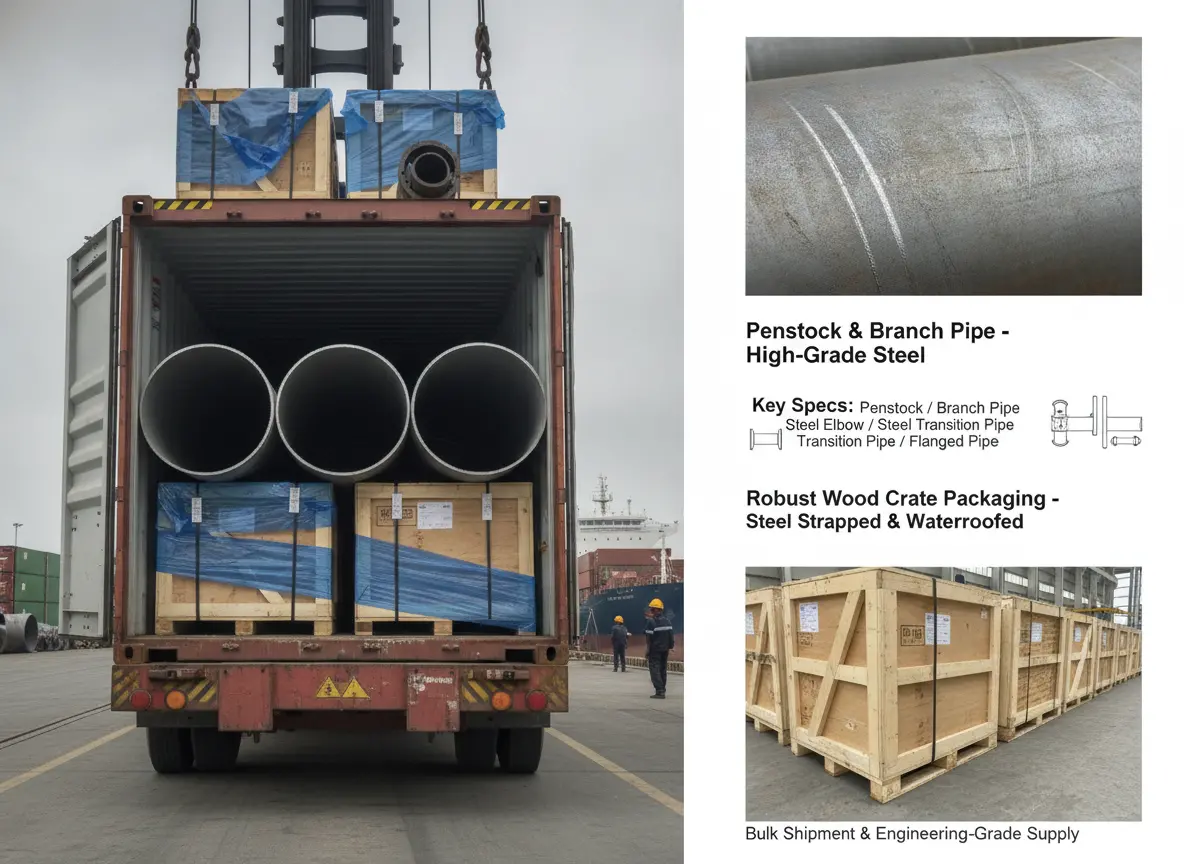
For international logistics, provide the destination, preferred shipping method, site unloading limits, maximum transport dimensions, and any route restrictions. Large-diameter sections may require nesting, split-shell delivery, special cradles, or breakbulk planning. Protective bracing should prevent distortion during lifting and sea transport, while coated surfaces need non-abrasive contact points and suitable end protection. Packaging and preservation recommendations can be reviewed at [[INTERNAL_LINK]].
Frequently Asked Questions About Steel Penstock Procurement
Q: What is the difference between a steel penstock and ordinary welded steel pipe?
A: A steel penstock is designed as part of a hydraulic pressure system and is normally customized for the project’s head, surge pressure, alignment, supports, branches, and turbine interfaces. Ordinary welded pipe may be supplied to standardized dimensions without the same project-specific structural analysis. Penstock procurement also commonly requires detailed fabrication drawings, qualified welding, defined NDT, coating documentation, and coordinated field-joint arrangements.
Q: Which steel grade should be used for a steel penstock?
A: There is no universal grade for every project. Selection depends on design stress, plate thickness, minimum temperature, toughness, weldability, forming requirements, corrosion allowance, and the governing code. ASTM A36/A36M, ASTM A516/A516M, EN 10025-2, and GB/T 1591 are among the standards that may be considered, but the project engineer must specify and approve the exact grade and supplementary requirements.
Q: Can a steel penstock be manufactured to a custom diameter and thickness?
A: Yes. Fabricated plate construction allows diameter, shell length, thickness, reducers, elbows, branches, and reinforcement to be adapted to the hydraulic and civil design. Manufacturability, plate availability, forming capacity, transport limits, and welding access must be checked before the dimensions are finalized. Thickness should come from approved calculations rather than a generic pressure table.
Q: What certificates and inspection records are available?
A: The documentation package depends on the purchase specification. It can include material test certificates, heat-number traceability records, welding qualifications, NDT reports, dimensional inspection records, coating reports, test records, and release notes. State the required certificate type, language, standard edition, third-party involvement, and document format in the inquiry. Certification not requested until after production may be difficult to reconstruct.
Q: What is the minimum order quantity for a custom steel penstock?
A: MOQ varies with section size, steel grade, total weight, fitting complexity, coating system, and required engineering work. A supplier may evaluate a single project lot, but forming setup, documentation, inspection, and logistics still influence commercial feasibility. Send the bill of quantities and drawings to obtain an order-specific MOQ instead of relying on a standard figure.
Q: How long does steel penstock production take?
A: Lead time is determined after reviewing drawings, materials, section sizes, inspection scope, coating, and current production loading. The schedule normally begins after technical clarification, commercial confirmation, and drawing approval. Material procurement, third-party witness points, coating cure time, and oversized-cargo arrangements may extend the total period, so these activities should be included in the agreed delivery program.
Q: What payment methods are normally accepted for export orders?
A: Available methods depend on order value, destination, credit assessment, production duration, and the seller’s commercial policy. International orders may use bank transfer, letter of credit, or another mutually agreed instrument. The quotation should define deposit or milestone requirements, document conditions, bank charges, currency, and the payment point linked to inspection or shipment. No payment structure should be assumed before written commercial confirmation.
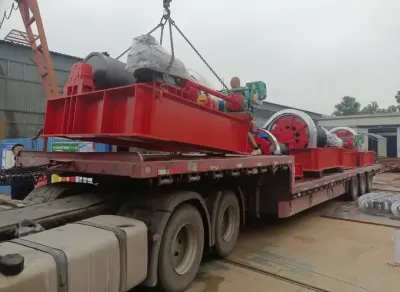
Q: How is a large-diameter steel penstock shipped internationally?
A: Shipment may use complete cylindrical sections, nested sections, split shells, or specially packed components. The choice depends on diameter, section length, coating sensitivity, container limits, vessel options, inland route restrictions, and site lifting capacity. Shipping cradles, internal braces, lifting marks, end covers, and moisture protection should be included in the packing plan. Oversized dimensions require logistics review before fabrication lengths are frozen.
Q: How are steel penstock welds inspected?
A: Inspection usually combines visual examination with specified non-destructive methods such as ultrasonic, radiographic, magnetic-particle, or penetrant testing. ISO 17635 provides general rules for NDT of metallic welds, while method-specific and acceptance standards must be stated by the project. The inspection percentage and acceptance level should reflect joint type, stress category, accessibility, and the governing design requirements.
Q: What information is needed for an accurate steel penstock quotation?
A: Provide diameter, length, design and transient pressures, steel grade or governing material standard, thickness schedule if already calculated, route drawings, fitting list, support concept, coating requirements, NDT scope, document requirements, delivery destination, and required schedule. Also identify field-joint responsibilities and maximum transport dimensions. More complete input allows the supplier to separate material, fabrication, inspection, coating, packing, and logistics assumptions clearly.
Request a Steel Penstock Quotation
Send your steel penstock drawings, hydraulic design conditions, bill of quantities, applicable standards, inspection plan, coating specification, delivery destination, and required completion date for a technical and commercial review. The quotation can then address material selection, fabrication scope, documentation, packing, logistics, MOQ, and lead time against the actual project requirements. Contact the manufacturing team through [[INTERNAL_LINK]] to request a tailored proposal for your hydropower, water transmission, pumped-storage, or industrial pressure-conduit project.
Ratings & Reviews
Know your supplier
Supplier's customization ability
- Drawing-based customization
- Sample-based customization
- Full customization
Minimum order quantity: 1 ton
Shipping total: To be negotiated
- Lead time:
- confirmed with the quotation
- Packaging:
- standard export packing
- Samples:
- available on request